China Die Making Steel Rule Manual Bender for Efficient Cutting and Creasing
2026-10-25
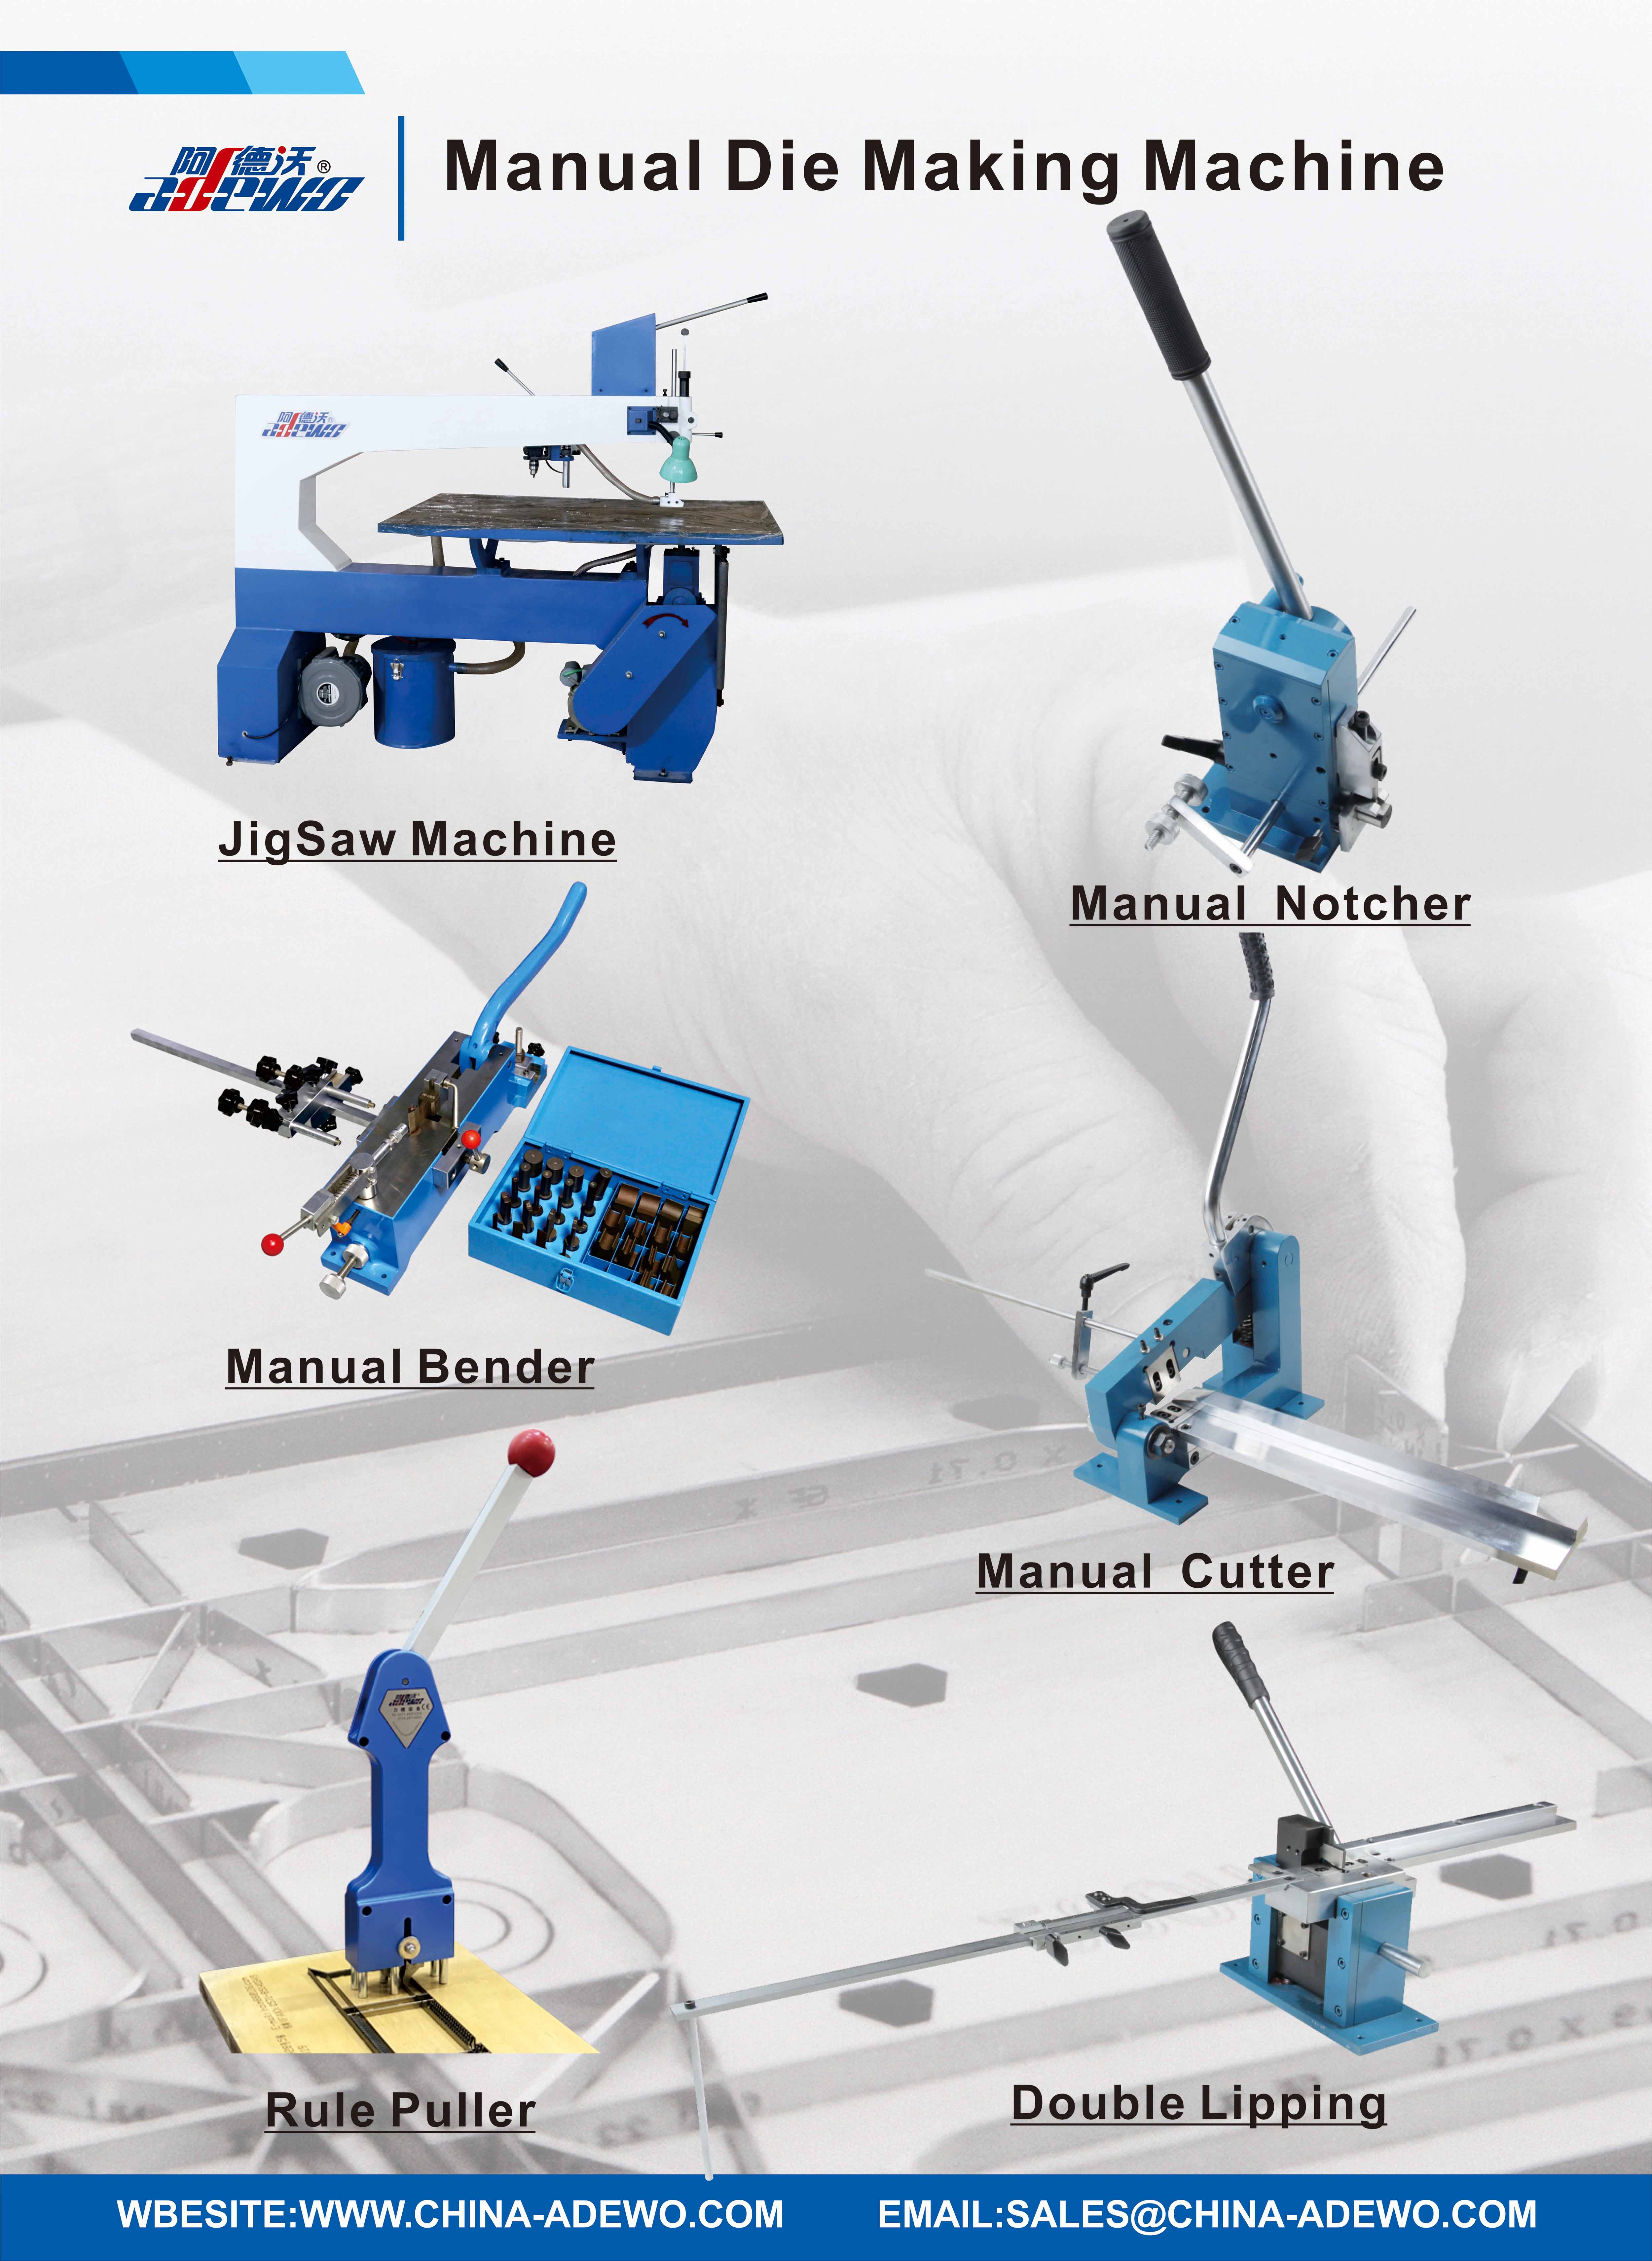
Ask any die maker what slows them down most, and the answer often comes back to one thing: bending steel rules by hand. It's tedious, imprecise, and eats up time that could be spent actually cutting and creasing. A manual bender built for efficiency can change that overnight. Meet the ADEWO China Die Making Steel Rule Manual Bender—a tool designed to turn a bottleneck into a breeze.
Why a Manual Steel Rule Bender Still Wins for Short-Run Die Work
When the job calls for a handful of cutting dies, not a thousand, the manual steel rule bender starts to look less like a relic and more like the smartest tool in the room. CNC benders shine on long runs where setup time amortizes into nothing, but short-run work punishes that math. You can program, fixture, and calibrate a machine for half an hour—or you can grab a hand bender and have the first rule bent before the CNC finishes booting. For a die that might cut a few hundred sheets total, the manual approach simply finishes sooner.
There is also a tactile advantage that automation cannot fake. A skilled operator feels the springback of the steel as it wraps around the former, adjusts pressure mid-bend, and sneaks up on a tricky angle without scrapping a strip. That feedback loop is instant and personal. Short-run die work is full of one-off profiles, odd radii, and last-minute changes; a manual bender lets you correct course on the spot instead of editing coordinates and rerunning a cycle. The tool becomes an extension of the hand, and the operator learns its quirks the way a machinist learns a favorite lathe.
Maintenance and floor space tell the same story. A manual bender has no servos to drift, no software updates to install, no encoder errors to chase down at 4 p.m. on a Friday. It sits in a corner, ready to work after a quick wipe-down. For a shop that runs a handful of custom dies each week, that reliability beats a high-tech machine that sits idle most days. The manual bender does not win because it is old; it wins because for short-run work, old is exactly what you need—simple, immediate, and honest.
The Connection Between Bend Accuracy and Cutting Performance
Bend accuracy rarely gets the credit it deserves until a cutting station downstream starts turning out scrap. When a tube or sheet is bent even half a degree off target, the cut line shifts—sometimes by millimeters, sometimes by enough to ruin a weld prep or leave a tab too short for fixturing. Operators on the floor know the pattern: you chase the blade alignment, swap inserts, re-zero the backgauge, but the real culprit sits two steps earlier in the bend cell. Springback and material variation don’t just alter the bend angle; they rotate the entire cross-section, so the programmed cut point no longer sits where the CAD model says it should. That mismatch forces the cutter to compensate on the fly, and compensation always costs edge quality or cycle time.
In high-mix shops, the link shows up most clearly when switching from one alloy batch to another. A 5052 aluminum blank behaves differently than a 6061 blank of the same thickness, and if the bend controller hasn’t been tuned for that lot’s actual yield strength, every cut after the bend inherits a slight twist or offset. The laser or saw doesn’t care about the bend’s intention—it only sees the material presented to it. So a bend that’s accurately formed but poorly positioned relative to the part datum will force the cutting head to re-probe, re-clamp, or worst case, re-cut a feature that was already supposed to be finished. That’s not a cutting problem; it’s a bend-to-cut handoff problem.
Some fabricators solve it by integrating in-process angle measurement during bending, then feeding the actual geometry to the cutting program in real time. That way the cut path adjusts to the real part, not the ideal one. The payoff isn’t just fewer rejects—it’s cleaner edges on the second operation because the blade or beam enters the material at the correct orientation instead of gnawing at a misaligned corner. Bend accuracy, in other words, quietly determines whether cutting performance gets judged by the part or by the scrap bin.
Adjusting the Tool for Different Steel Rule Thicknesses
The tool's clamping jaw has a spring-loaded stop that sits just above the rule seat. To switch from a 0.5 mm thick steel rule to a 1.0 mm rule, back off the two hex screws on the side plate until the jaw floats freely, then slide the correct spacer (marked with the target thickness) into the slot behind the jaw. This keeps the cutting edge square without over-tightening.
For older units without the spacer channel, use the knurled adjustment collar under the handle. Turn it clockwise until the rule can be inserted with light friction, then give it an extra quarter turn. A quick test cut on scrap material will show if the rule shifts; if it does, add another eighth of a turn. Avoid cranking past the red line on the collar, as that bends the rule and dulls the blade prematurely.
If you regularly switch between metric and imperial rules, consider marking your most used settings with a paint pen on the side plate. Wipe the seating area with a dry cloth before each change—metal dust from previous cuts can make a thin rule sit slightly proud and throw off the alignment.
Avoiding Common Mistakes That Cause Rule Cracking or Distortion
Most rule cracking and distortion start with how the rules are handled before any pressure is applied. A frequent mistake is forcing a strip into place when the surface isn’t clean or dry—dust, oil, or even a thin layer of moisture can create uneven stress points that later turn into hairline fractures. Instead of pushing the rule flat with one hand while tightening with the other, lay it gently and let the adhesive or fasteners do the holding. If you’re using a steel rule, avoid bending it back and forth to “test” flexibility, as repeated micro-flexing weakens the temper along the edge.
Another overlooked trigger is inconsistent clamping pressure. When you tighten one end fully before the other, the rule bows slightly, and that bow becomes permanent once the material cools or the adhesive sets. Work in a diagonal pattern, applying just enough force to hold position without squeezing out the bonding layer. For rules with pre-punched holes, never enlarge a hole with a drill bit while the rule is mounted—the heat and vibration travel along the grain and can start a crack at the next stress riser. Remove the rule, make the adjustment, then reinstall with fresh alignment.
Finally, watch how the rule meets the workpiece. Slamming a rule against a hard stop or using it as a scraper or pry bar invites distortion that no amount of straightening will fully correct. Keep the contact edges clean and burr-free, because even a tiny nick concentrates force and leads to local bending. If a rule starts to show a slight wave or a shiny crease, retire it from critical measuring tasks immediately—small distortions grow fast under repeated load, and a cracked rule can fail without warning.
Maintaining a Chinese-Built Manual Bender for Consistent Creasing
Most wear on a Chinese-built manual bender shows up first at the hinge pins and the creasing channel. I brush out paper dust and tiny metal flakes from the lower die after every longer run, then wipe the male die with a dry cloth. If you let that grit sit, it changes the crease depth on one side and you end up chasing settings instead of working.
Check the two depth-adjustment screws before each job, not just when the crease starts looking weak. On many of these machines the lock nuts back off slightly after the first week of use, so a quick snug with a wrench keeps the beam from tilting. A thin film of light machine oil on the pivot points is enough; anything heavier attracts dust and makes the handle feel sticky.
For consistent creasing, set the depth with a scrap strip from the same batch rather than relying on the scale printed on the side. Once the crease looks right, mark the position of the adjustment collar with a pencil line so you can return to it after cleaning or changing dies. If one end starts creasing deeper than the other, loosen the die bolts and reseat the female channel before touching the depth screws.
From Flat Rule to Finished Die: A Practical Bending Sequence
Starting with a flat rule, the first thing to nail down is the actual bend allowance for your material thickness and tooling. Don't trust generic charts blindly—grab a scrap piece, mark a known length, put it through the brake, and measure the resulting leg lengths. That measured difference becomes your real-world K-factor, and it will save you from chasing impossible dimensions later in the sequence.
Once the flat pattern is locked, order your bends by considering tool access and part geometry. Always start with the bends that keep the part as flat and stable as possible on the die—typically the outer or perimeter bends before the internal ones. If a bend will trap the part against the punch or cause the already-formed flanges to collide with the machine frame, it needs to move later. Simple rule: bend from the outside in, and from the largest flange to the smallest.
Finally, check your die clearance and punch radius before each hit, not just on the first piece. A practical sequence isn't just about geometry; it's about repeatability. Use backgauge stops on every bend that can accept them, and if you're working with a press brake, make sure the part is supported with your hands or a follower so it doesn't sag between hits. When the last bend closes and the part drops off the tool without forcing, you've turned that flat rule into a finished die—accurate, consistent, and ready for the next one.
FAQ
It handles standard steel rule from 0.71mm to 1.05mm thickness, and the bending head accepts heights up to 23.8mm, which covers most die making jobs for packaging and labels.
With a well-calibrated bender and a steady hand, you can hit consistently tight radii and sharp bends. It's not as fast as CNC, but for custom or low-volume die boards the control is actually very direct and repeatable.
Yes, the same bending mechanism works for both cutting and creasing steel rule. You just swap in the appropriate rule height and profile; the manual settings let you adjust the angle without changing tooling.
It's ideal for small to mid-size die making shops, packaging prototype labs, or in-house converting departments that need to produce or repair flatbed dies without investing in heavy automated equipment.
Keep the bending head and guide rails free of steel dust and oil them lightly after each shift. Check the clamping bolts for wear monthly, and re-calibrate the angle stop every few months if you notice drift.
Basic training takes about half a day. Someone familiar with die board layout can pick it up quickly because the manual lever gives you tactile feedback on how the rule is forming. It's more about feel than complex programming.
You can expect to cut bending time roughly by half for typical die layouts. Because the bender holds the rule firmly and gives consistent angles, you also get fewer rejected bends and less rework on the die board.
Conclusion
For small-batch die work, a manual steel rule bender from Chinese manufacturers often outperforms automated alternatives simply because it allows immediate, tactile adjustments without reprogramming. The tool's leverage point and angle stop need to align precisely with the rule's temper; a slight deviation in bend radius translates directly into inconsistent cutting depth or crease width on the final sheet. Operators who take time to measure the actual rule thickness—commonly 0.71 mm, 1.05 mm, or 1.42 mm—can set the gap and bending nose accordingly, preventing the rule from slipping or deforming. This attention to dimension matters more than raw speed, especially when running short orders where a ruined rule costs more than the time saved.
Cracking and distortion usually stem from forcing a cold rule through too tight a radius or from a dull bending nose that digs into the metal. A properly maintained Chinese-built bender keeps its pivot pins lightly oiled and its clamping faces free of zinc or paper residue, which otherwise cause uneven pressure and micro-fractures. When moving from flat stock to a finished die, a practical sequence starts with the longest straight sections, then works outward to the corner bends, checking each angle against a sample crease line before proceeding. This stepwise approach reduces rework and preserves the rule's spring temper, so the finished die produces clean cuts and crisp creases even after hundreds of impressions.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com